 OK
The time the line is stopped
Breakdowns, format changes, waiting for material. We know when, how long and why.
Home / Software / OEE, downtime and waste
Production data · OEE
Almost every line produces less than it could, and the cause is seldom known with certainty. We measure how much your line produces, how long it stands still and how much product is discarded, and we present it in a report you can read in five minutes.
What we do
We connect to the line's PLC and to the systems you already have, collect running time, stops and rejects, and turn them into figures anyone can understand: how much was made, how much was discarded and how long the line was stopped, and why.
What OEE is
OEE (overall equipment effectiveness) sums up in one percentage how much of what your line could produce actually comes out good. Behind it are three different losses, and each one is tackled differently.
Breakdowns, format changes, waiting for material. We know when, how long and why.
Micro-stops and speed below nominal: the loss that is hardest to see.
Rejects and waste counted at every point of the line, so you know where they start.
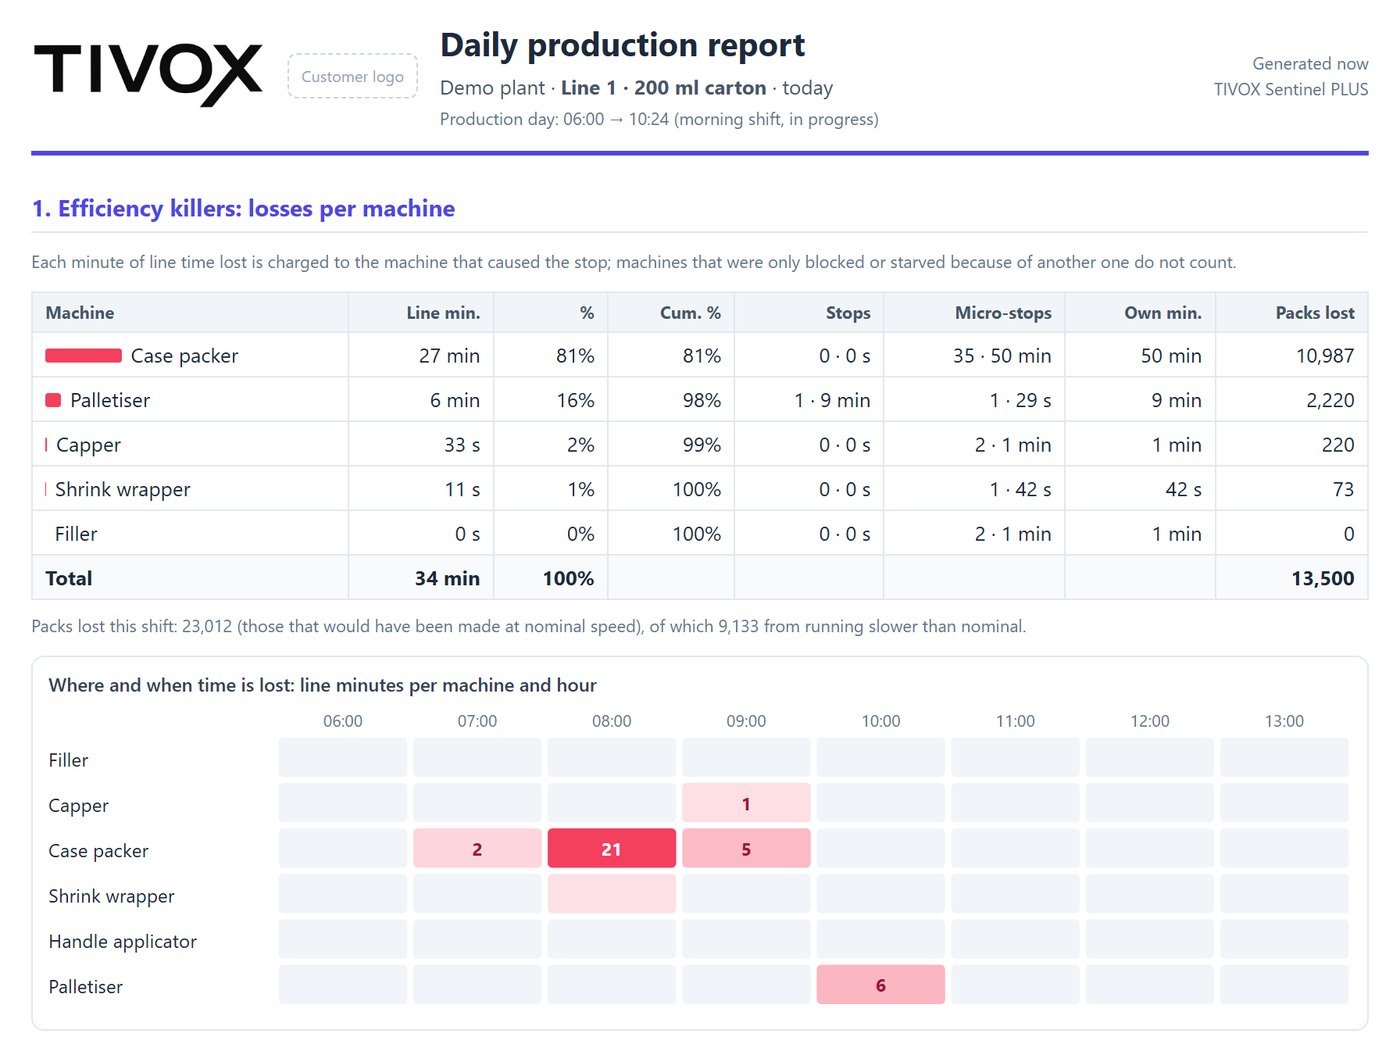
New · OEE per machine
Line OEE tells you how much you lose; machine OEE tells you where. With photocells between machines we know which one stopped by itself and which were only starved or blocked, and every morning the efficiency-killers report arrives: the Pareto of line minutes lost per machine, micro-stops versus stops, an hourly map and the packs lost.
OEE by day · line 2 · %
On Tuesday line 2 was stopped for 1 h 52 min: 1 h 10 min for a format changeover that overran and 42 min of micro-stops at the labeller. Without that changeover, OEE would have been 77%.
Source: line 2 stops on Tuesday and the changeover log
Mock-up with demo data.
How we start
FAQ
There is no single figure that suits every line: it depends on the product, the format and how many changeovers you make each day. What helps is measuring your line with the same rule, shift after shift, seeing which of the three losses costs you most and checking that it goes down week after week. That is why we measure first, before promising any target.
It is overall equipment effectiveness: it multiplies availability (running time), performance (actual speed versus nominal speed) and quality (good product versus total). An OEE of 100% would mean always running, at full speed, without discarding anything.
No. We connect to what you already have and, if a signal is missing, we add only the minimum needed.
The data is yours and stays in your plant. The cloud only receives what you decide.
Yes, and that is what we recommend: start with the line that worries you most, measure it and expand from there.
That, of everything the line could produce in the planned time, 85% comes out as good product; the rest is lost to stops, running below rated speed or scrapped product. 85% is often quoted as a world-class benchmark, but what matters is comparing your line with itself: knowing which of the three losses weighs most and bringing it down.
With three columns per shift: availability (run time ÷ planned time), performance (units produced × ideal cycle time ÷ run time) and quality (good units ÷ units produced). OEE is the product of the three. The weak point of a spreadsheet is that it depends on someone logging stops by hand; our OEE demo shows what it looks like when it is measured automatically.
Let's talk about your plant
Tell us which line worries you. We will suggest how to measure it and where to start improving.