 OK
Pack without a cap
The pack has gone through without a closure and must not leave the line.
Home / Machine vision / Caps and closures
Pack integrity · machine vision
A missing cap, one sitting high or skewed, or a broken tamper seal won't show up in the hourly sample. They show up if you look at every unit. With machine vision we check the closure of every pack at line speed, and any pack that fails is rejected along with its photo.
What it does
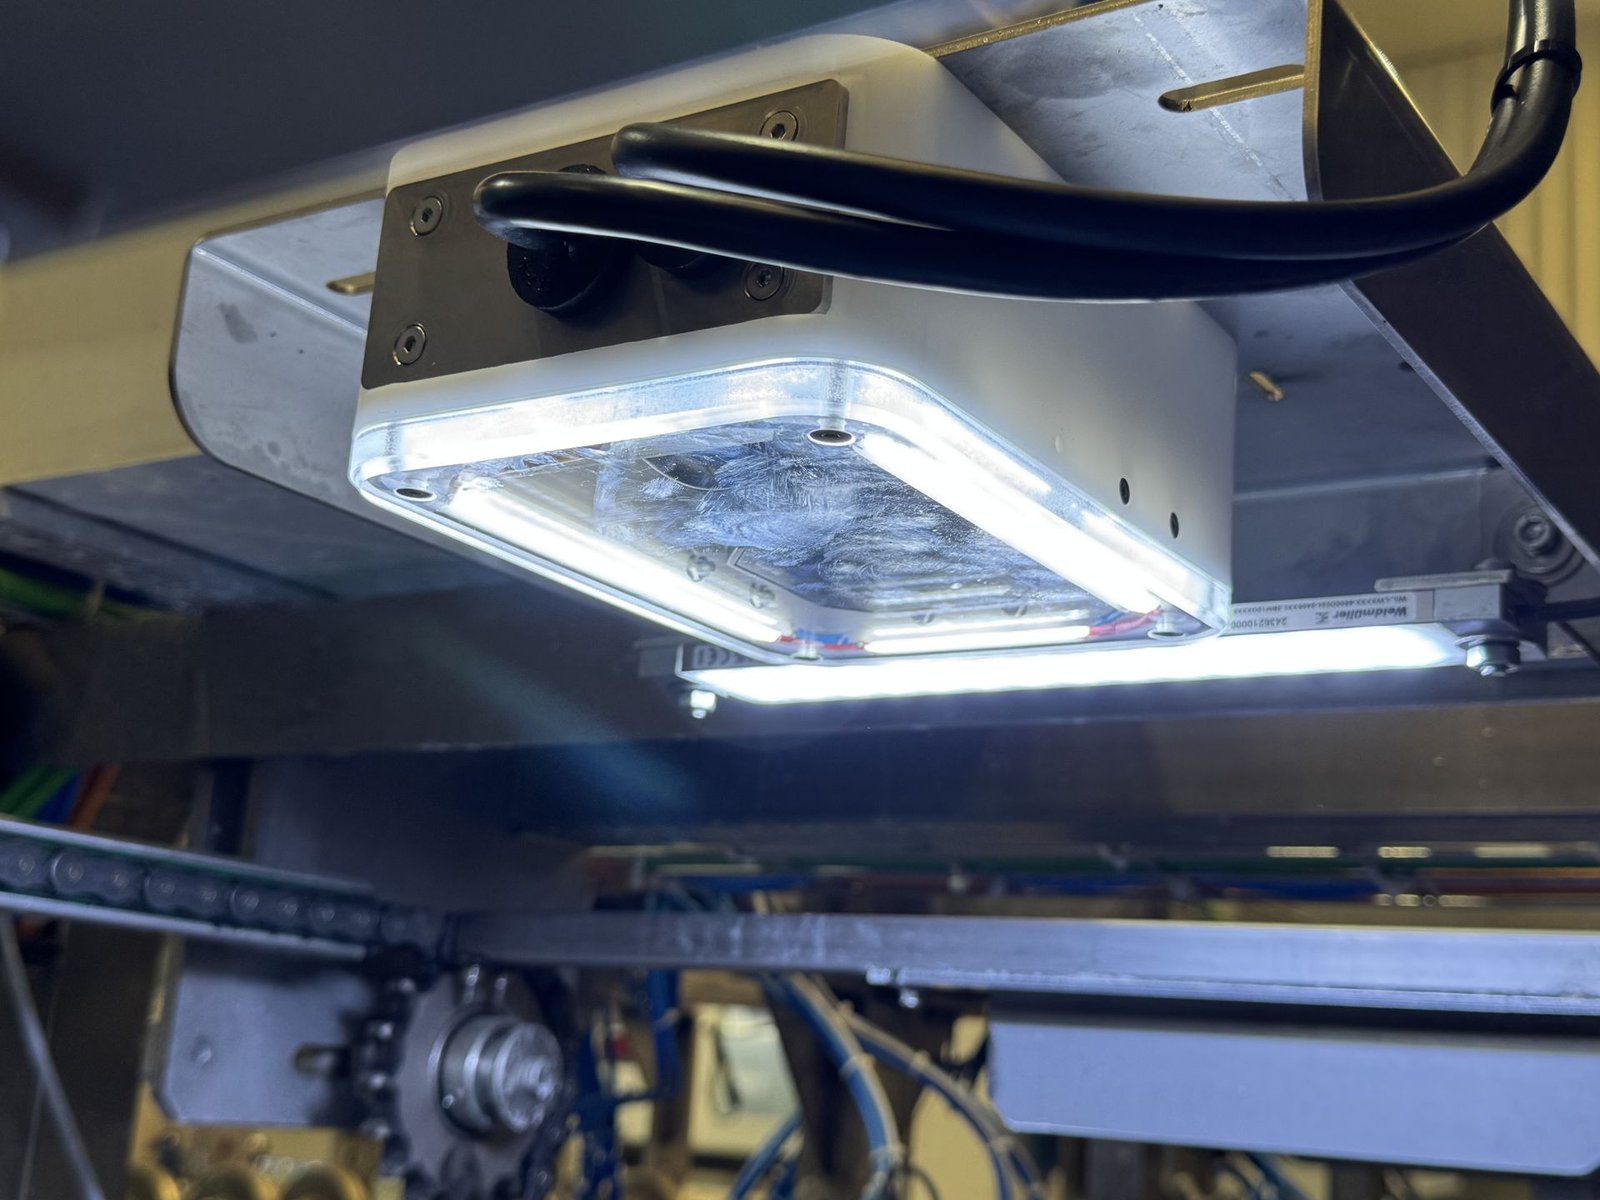
A HIKROBOT smart camera looks at the closure of every pack and compares it with the recipe for that format. If any measurement falls out of range, the pack is rejected and its image is stored with the exact reason.
What we detect
These are the closure checks we install most often. If your defect isn't on the list, we'll run a feasibility test free of charge.
The pack has gone through without a closure and must not leave the line.
The cap is on, but it hasn't gone all the way down.
Centring and skew measured on every pack, against the threshold in your recipe.
That the tab is there and the tamper-evident seal is intact.

How it's built
The camera sees, the trigger decides when, the recipe sets the verdict, the rejector acts and the log keeps the record. We tune it on your line, with real product.
The same inspection can also check the date and batch coding or the label and codes, depending on where they are on the pack.
FAQ
Missing cap, high, off-centre or skewed cap, and the opening tab and tamper seal. All on 100% of packs, in line, with a photo of every reject.
We check first with a feasibility test at no cost, using your good and bad packs. We tell you whether it can be detected in line, with which technique and with what reliability to expect; what cannot be guaranteed, we tell you up front.
They are removed from the line, and every reject is stored with its photo, time, recipe and reason, available to quality and for any audit or complaint.
No. Each format has its own recipe, and changing over means loading another one, in seconds.
Free feasibility test
Send us photos of a good pack and a bad one, or real samples. We'll tell you whether it can be detected in-line and with what expected reliability. Whatever we install, we guarantee.